Strawberry quality is decided in the 30 minutes between truss and punnet. Greenhouse berries that reach retail at 90 per cent marketable yield were picked at the correct colour stage, cooled within 30 minutes, and never stacked above four punnets. Conversely, fruit picked red-deep at midday and left in a 25 degree picking tray loses three days of shelf life. The picking and packing protocol is a climate-controlled workflow as much as a hand-harvest operation.
Maturity Indices and Pick Window
Greenhouse strawberry for local direct market is picked at 75 to 80 per cent surface red; for long-distance wholesale, 60 to 70 per cent red. The colour standard is matched against a colour-card set: stage 3 is 70 per cent red, stage 4 is full red. A berry picked below stage 3 never develops full flavour; a berry picked above stage 4 bruises easily. Calyx attachment is also checked: the cap should remain green and turgid at picking, not browned.
Pick frequency is every 2 to 3 days in warm weather and every 4 days in cool weather. The best picking window is early morning, 2 to 4 hours after sunrise, when fruit is at 12 to 15 degrees Celsius. Picking after midday heat pushes fruit temperature above 25 degrees, removing any chance of 5-day shelf life. A single picker harvests 15 to 25 kg per hour; moving too fast causes green-underneath fruit to slip into the tray.
Harvest Handling and Pre-Cooling
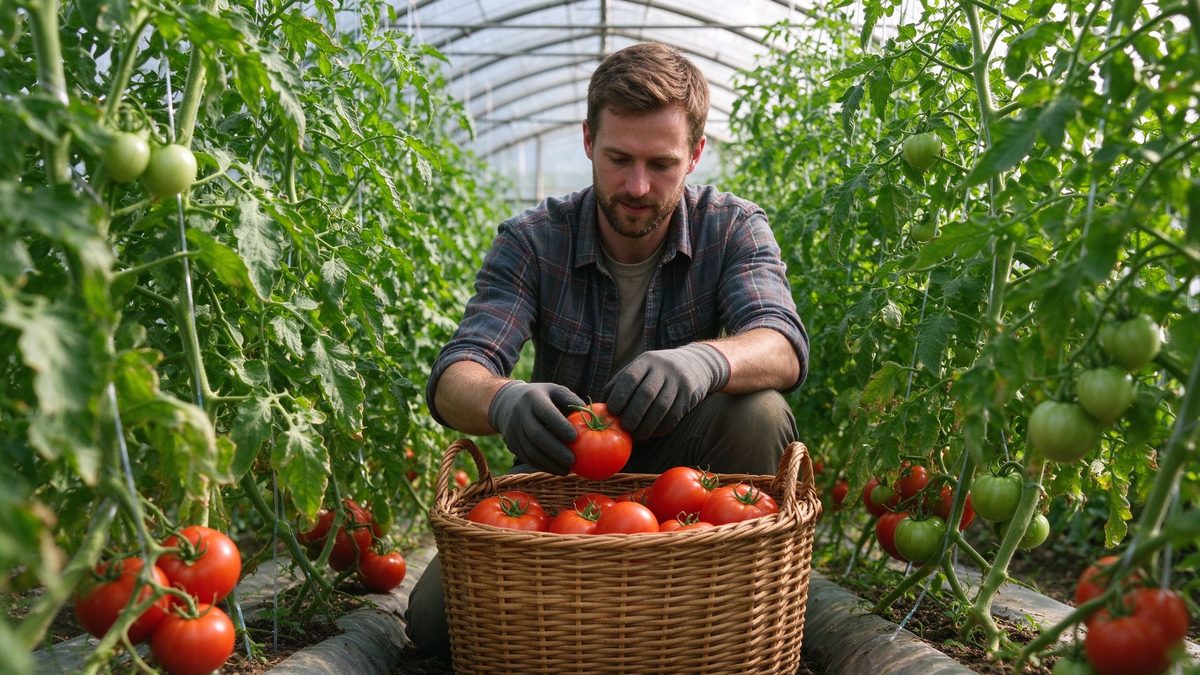
Pickers use a twist-and-pull motion that leaves the cap on; fruit is never yanked off the truss. Berries are placed directly into 250 g or 500 g punnets, never into bulk buckets, because bruising from stacking multiplies. Punnets go immediately into a shaded trolley, and trolleys move to the packhouse within 15 minutes of leaving the bay. A cool chain that holds below 7 degrees from packhouse onward doubles shelf life.
Forced-air pre-cooling brings fruit from 20 degrees down to 2 degrees within 30 to 45 minutes. The cooler operates at 0 to 2 degrees Celsius with 95 per cent relative humidity and a 0.5 to 1.0 m/s airflow across vented punnets. Forced-air tunnel coolers pull air through cartons with a 50 Pa pressure differential; this is far faster than room cooling, which takes 4 to 6 hours and allows mould to start. Punnets are then moved to a 1 degree cold store awaiting dispatch.
Packing, Grading, and Traceability
Punnets are conveyed on a sorting line where cameras or hand graders check size, colour, and defects. Grade 1 fruit is 22 g or heavier with no blemishes; Grade 2 is 18 to 22 g or minor cosmetic. Cartons hold 12 punnets and are stacked no more than 4 high in cold storage to avoid crushing bottom layers. Labels carry lot code, pack date, and greenhouse bay number, enabling traceability back to a single picking shift.
Packhouse hygiene is audited weekly. Floors are washed with 200 ppm chlorine every shift; sorting lines are sanitised at lunch and end of day. Workers wear single-use gloves and hairnets; anyone with a cut on the hand is reassigned away from fruit contact. These steps sound bureaucratic but they are the difference between a clean microbiological test at retail and a rejected consignment. Zhongtian Agricultural Technology applies the same HACCP-style checklist across all contracted bays.
Cold Chain and Retail Shelf Life
Dispatch trucks are pre-cooled to 2 degrees before loading; loading completes within 20 minutes so fruit does not re-warm. Insulated pallet covers hold temperature within 1 degree during road transport. At retail, display counters hold fruit at 4 to 6 degrees, never on ice directly, because wetting accelerates grey mould. A well-handled punnet holds 5 to 7 days of shelf life; a poorly handled one lasts 2 days.
Post-harvest losses are tracked weekly by lot. Each batch that returns from retail with more than 10 per cent mould is reviewed: pick timing, pre-cooling duration, and transit temperature are reconstructed. Common failure patterns show up quickly — a single bay with higher mould means Botrytis was building in the truss, not at the packhouse. Closing this feedback loop between retail and the greenhouse is how top growers lift from 80 per cent to 95 per cent marketable yield.
Picking and packing are the final quality gate. Picking at the right colour stage in cool morning hours, forced-air cooling within 30 minutes, and a cold chain held at 1 to 4 degrees transform a technically good crop into a premium consignment. Every minute fruit spends above 10 degrees after picking comes out of shelf life; treating that minute as money is the discipline that separates market leaders from average producers.